
Technical Concentrate for Agrochemical Formulation & Manufacturing
Technical Concentrates comprise high-purity active botanical, enzymatic, and biochemical raw materials processed for industrial formulation. Supplied in standardized powder or liquid extract forms, these raw materials serve as the core active components in dietary supplements, functional foods, and cosmeceutical formulations. Every batch undergoes high-performance liquid chromatography (HPLC) verification to guarantee consistent active marker compound percentages for secondary manufacturing.
-
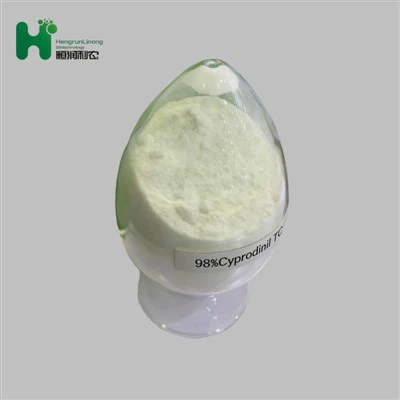
![Cyprodinil 98% TC]() Cyprodinil 98% TCActive Ingredients: Cyprodinilview more
Technical Grade: 98% TC
CAS: 121552-61-2
Registration: PD20182808
Appearance: White to off-white crystalline solid
Certificates:... -
![Fenhexamid 98% TC]() Fenhexamid 98% TCActive Ingredients: Fenhexamidview more
Technical Grade: 98% TC
CAS: 126833-17-8
Registration: EX20210157
Appearance: White to off-white crystalline powder ... -
![Quinoxyfen 98% TC]() Quinoxyfen 98% TCActive Ingredients:Quinoxyfenview more
Technical Grade: 98% TC
CAS:124495-18-7
Registration:EX20240293
Appearance: White to off-white crystalline... -
![Spiroxamine 95% TC]() Spiroxamine 95% TCActive Ingredients:Spiroxamineview more
Technical Grade: 95% TC
CAS:118134-30-8
Registration:EX20220072
Appearance: Light brown oily liquid
Certificates:GLP 5... -
![Pyriproxyfen 98% TC]() Pyriproxyfen 98% TCActive Ingredients:Pyriproxyfenview more
Technical Grade: 98% TC
CAS:95737-68-1
Registration:WP20120041
Appearance: White to light yellow crystalline... -
![Flusilazole 95% TC]() Flusilazole 95% TCActive Ingredients:Flusilazoleview more
Technical Grade: 95% TC
CAS:85509-19-9
Registration:PD20085601
Appearance: White to light beige crystalline powder
Certificates:5... -
![Fludioxonil 98% TC]() Fludioxonil 98% TCActive Ingredients:Fludioxonilview more
Technical Grade: 98% TC
CAS:131341-86-1
Registration:PD20152053
Appearance: White to off-white crystalline powder
Certificates:5...


Product Range
Standardized Botanical Concentrates:
High-assay herbal active extracts (e.g., Curcumin 95%, Ginseng Saponins 80%, Berberine HCl 97%) processed via ethanol/water extraction.
Enzymatic & Microbial Concentrates:
Fermentation-derived active enzymes and microbial metabolites scaled for bulk nutritional and industrial blending.
Cosmetic Active Concentrates:
Purified active molecules (e.g., Asiatic Acid, Polydatin, Resveratrol) formulated for topical emulsion and serum integration.
Custom Assay Blends:
Formulations adjusted to specific client titer requirements, carrier ratios, and solubility parameters.
Technical Parameters
|
Parameter Category |
Specification Range |
Test Method |
|
Active Assay (Titer) |
40% - 98% (Compound Specific) |
HPLC / UV-Vis |
|
Loss on Drying |
<= 5.0% |
Gravimetric (105 deg C, 3h) |
|
Ash Content |
<= 1.0% |
USP <281> Ignition |
|
Heavy Metals |
Lead (Pb) < 0.5 ppm, Arsenic (As) < 0.3 ppm |
ICP-MS |
|
Microbial Limits |
Total Plate Count < 1000 CFU/g, Yeast/Mold < 100 CFU/g |
ISO 4833 / USP <2021> |
|
Particle Size |
95% through 80 Mesh |
Sieve Analysis |
Application & Formulation
Dietary Supplements:
Encapsulated and tableted raw materials requiring strict bulk density (0.45 - 0.65 g/ml) and direct compression flowability.
Functional Beverages:
Water-soluble liquid and powder concentrates engineered for clear dissolution without sedimentation or cloud point interference.
Cosmeceutical Emulsions:
Active concentrates dissolved in biocompatible glycols or aqueous bases for anti-aging and barrier-repair creams.
Dosage Integration:
Raw material titers calculated to match target finished-product label claims while minimizing excipient load.
Manufacturing Capability

Extraction Infrastructure:
Multi-stage stainless steel extraction tanks (5,000L capacity) operating under controlled negative pressure and low-temperature evaporation to preserve heat-sensitive active compounds.
Purification & Separation:
Industrial chromatography columns and membrane ultrafiltration systems designed to remove residual plant waxes, chlorophyll, and inorganic salts.

Drying Systems:
Low-temperature vacuum belt drying and centrifugal spray dryers equipped with automated inlet/outlet temperature controllers to prevent thermal degradation.
Batch Capacity:
Annual output capacity exceeding 1,200 metric tons across standard botanical and biochemical active lines.
QC & Documentation
In-House Analytical Laboratory:
Equipped with Agilent HPLC systems, gas chromatography-mass spectrometry (GC-MS), and atomic absorption spectroscopy (AAS) for real-time batch testing.
Third-Party Verification:
Random split-sample testing conducted via ISO 17025 accredited laboratories (SGS, Eurofins) prior to final export clearance.
Traceability Documentation:
Every shipment includes a batch-specific Certificate of Analysis (COA), Material Safety Data Sheet (MSDS), pesticide residue report, and non-GMO statement.
Supply / OEM
Minimum Order Quantity (MOQ):
25 kg fiber drum standard packaging (customized sample sizes available from 500g for R&D evaluation).
Packaging Configuration:
Food-grade double low-density polyethylene (LDPE) inner liners sealed inside heavy-duty cardboard fiber drums with tamper-evident locking rings.
OEM Customization:
Tailored assay adjustments, carrier selection (maltodextrin, rice flour, or pure excipient-free delivery), and private label drum marking.
Logistics & Storage:
Temperature-controlled warehousing maintaining dry, dark conditions below 25 deg C with global air and ocean freight export compliance.
Our Certificate


FAQ
We're well-known as one of the leading technical concentrate manufacturers and suppliers in China, featured by quality products and low price. Please rest assured to buy discount technical concentrate from our factory. Welcome to view our website for more information.
technical concentrate, Fludioxonil 98 TC, Cyprodinil 98 TC